Table of Content
Industrial dual-shaft shredders excel at volume reduction and pre-shearing for sheet metal, auto body panels, and light iron, but feeding unshreddable solid driveline components causes catastrophic mechanical failure. A dual-shaft shredder handles sheet gauge metals, empty auto bodies, appliances, and stamping scrap up to 3 to 4 mm thickness, but solid steel shafts, cast iron gearboxes, and structural billets require heavy pre-shredders or hydraulic shears. Below, I break down acceptable light iron streams, uncrushable components that destroy shredder shafts, and how to determine whether your volume and scrap mix require a larger industrial shredder.

What Light Iron and Automotive Components Can a Dual-Shaft Shredder Safely Process?
Industrial dual-shaft shredders operate at low rotational speeds and high torque, using hooked alloy knives to grip, rip, and fold ductile scrap. Dual-shaft shredders safely handle sheet steel under 3 to 4 mm thickness, automotive doors, body skins, white goods, stamped skeleton, and bicycles, producing dense strips for downstream sorting.
Acceptable Feedstock: Light Iron, Sheet Metal, and Auto Body Panels
Industrial dual-shaft shredders (low-speed, high-torque shearing machines) are engineered primarily to tear, pierce, and fold ductile, hollow, and thin-gauge materials. In scrap yard operations across North America and Europe, they serve as the workhorse for high-volume size reduction before downstream sorting.
Standard Allowable Scrap Feeds
Dual-shaft shredders operate reliably on several primary light iron streams: – Automotive Sheet and Body Enclosures: Skinned vehicle doors, hoods, trunk lids, quarter panels, and unibody roof sections. The rotating hooked knives easily grip the thin sheet (typically 0.8 mm to 1.5 mm thickness), piercing and ripping it into manageable strips. – Consumer White Goods and Light Gauges: Washing machine housings, dryers, refrigerators (with refrigerants safely evacuated beforehand), sheet steel shelving, and HVAC ducting. – Industrial Stamping Skeleton and Clippings: Baled or loose punch-press skeleton, edge trimmings, light drum containers, and steel strapping. – Bicycles and Light Structural Tubing: Bicycle frames, thin-wall electrical conduit, and hollow furniture tubing with wall thicknesses under 3 mm (1/8 inch).
Because dual-shaft shredders operate at low rotational speeds (typically 12 to 25 RPM), they tear and compress scrap rather than pulverizing it by high-speed kinetic impact. This produces dense, folded strips ideal for feeding downstream magnetic separators or stationary shears. For driveline comparison, see our engineering guide on gearbox drive vs hydraulic drive dual-shaft shredders.
What Uncrushable Solid Hazards Cause Catastrophic Tooth Breakage and Shaft Runout?
The most frequent cause of catastrophic shaft failure, tooth shearing, or planetary reducer breakdown in scrap yards is feeding uncrushable solid components hidden inside light iron. Engine blocks, transmission housings, solid drive axles, structural I-beams, leaf springs, and pressurized gas cylinders must never enter a dual-shaft shredder.
Uncrushable Hazards: Solid Parts That Destroy Shredder Shafts
When an unyielding solid piece of steel enters the cutting chamber, the machine’s rotating knives cannot penetrate the metal. Instead, shaft rotation halts within milliseconds, generating destructive bending stresses:
Severe Contaminants and Un-shreddables
The following materials must be strictly sorted out before scrap enters a standard dual-shaft shredder: – Solid Automotive Driveline Parts: Engine blocks (cast iron or aluminum with pressed-in steel liners), solid cast transmission cases, forged crankshafts, vehicle axles, drive shafts, leaf springs, and brake drums. Solid steel shafts exceeding 20 mm (3/4 inch) in solid diameter do not yield under low-speed knife shear; they act as an unyielding wedge. – Heavy Structural Steel and Billets: Solid I-beams, steel plate thicker than 6 mm (1/4 inch), reinforcing rebar bundles, and crane counterweights. – Hardened Wear Components: Excavator bucket teeth, bulldozer cutting edges, ball bearings, and leaf springs made from high-tensile spring steel (such as 5160 steel). – Pressurized Gas Vessels: Unpunctured propane cylinders, vehicle shock absorbers, hydraulic struts, and fire extinguishers, which cause explosive rupture upon knife puncture.
| Scrap Component | Dual-Shaft Suitability | Operational Risk / Consequence | Recommended Alternative Processing |
|---|---|---|---|
| Auto body skin and doors | Excellent | Smooth shearing, low wear | Dual-shaft shredder |
| White goods and appliances | Excellent | Rapid compaction and tearing | Dual-shaft shredder |
| Solid automotive axle | Strictly Prohibited | Tooth spalling, broken shaft, stripped gearbox | Hydraulic alligator or guillotine shear |
| Cast engine block | Strictly Prohibited | Hydraulic relief lockup or mechanical shock fracture | Engine breaker or heavy hammer mill |
| Sheet skeleton under 3 mm | Excellent | High throughput, dense shred output | Dual-shaft shredder |
| Solid structural I-beam | Strictly Prohibited | Severe knife deflection, frame cracking | Heavy mobile or scrap shear baler |
Mechanical Consequences of Ingestion: Teeth, Shafts, and Reducers
- Knife Hook Spalling and Breakage: As the hooked tooth attempts to shear unyielding hardened steel, bending stress concentrates at the hook root, causing brittle tooth fracture.
- Hexagonal Shaft Deflection: Solid wedges exert radial forces exceeding several hundred kilonewtons. Permanent shaft runout creates knife-to-knife interference and rapid seal destruction.
- Planetary Reducer Gear Stripping: Motor rotor kinetic inertia slams into the high-ratio gearbox before electrical breakers can disconnect power, stripping gear teeth.
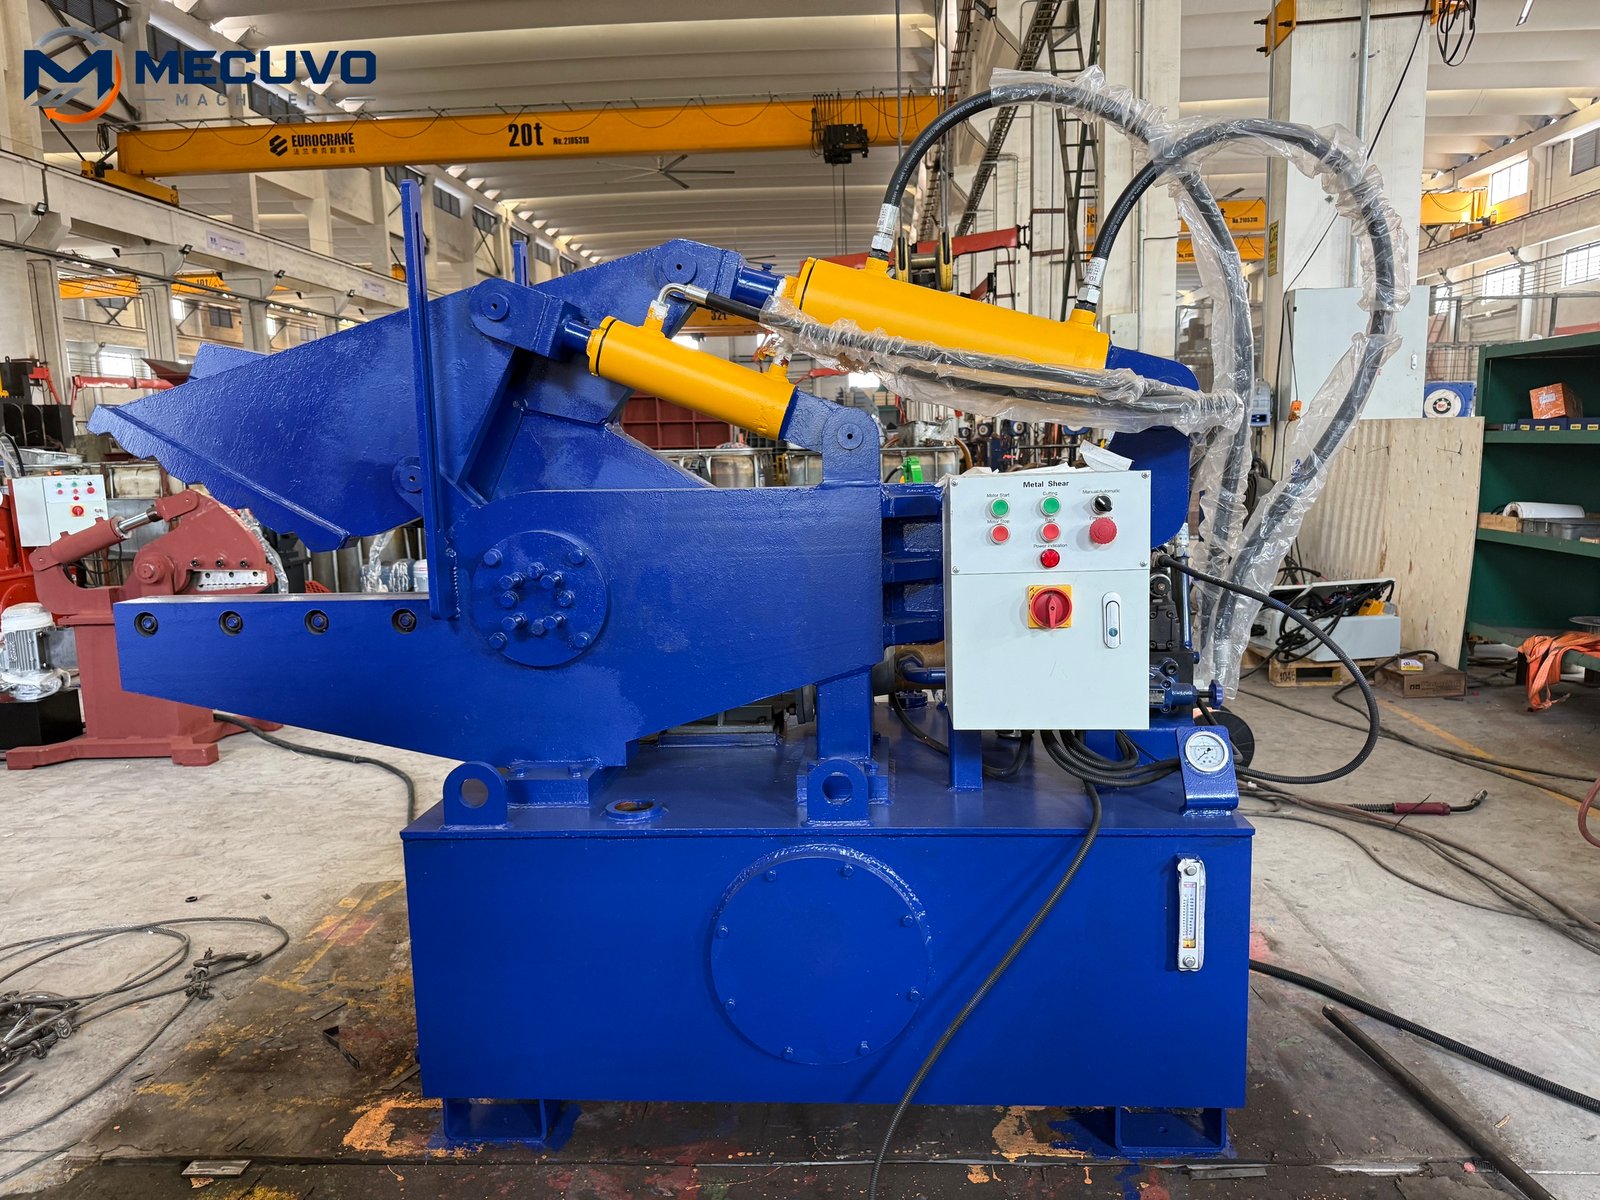
If your yard routinely handles heavy structural shapes alongside light sheet, compare machine capabilities in our overview of alligator shear vs guillotine shear vs shear baler.
When Does Scrap Volume and Material Thickness Require a Heavy Industrial Pre-Shredder?
Determining whether your yard can operate with a compact dual-shaft shredder or requires a heavy industrial pre-shredder depends on four primary parameters. Yards processing intact vehicle hulks, plate exceeding 6 mm, or volumes over 10 tons per hour require heavy pre-shredders with wider chambers and 110 kW to 200 kW power packages.
Sizing Thresholds: Chamber Dimensions, Drive Power, and Upstream Preparation
Selecting the proper machine envelope prevents costly bottlenecking and unplanned maintenance downtime:
1. Infeed Chamber Dimensions vs Whole-Body Processing
If your scrap stream consists of sheared car pieces, loose appliances, and light sheet scrap, a cutting chamber length of 1,200 mm to 1,600 mm is adequate. However, if your yard receives whole, intact automobile hulks, flattened car bodies, or high-cube commercial scrap, you require a heavy pre-shredder with an infeed opening exceeding 2,000 mm to 2,500 mm to prevent material bridging across the hopper.
2. Material Thickness and Drive Power
- Up to 3 mm Light Iron: Standard dual-drive shredders (30 kW to 75 kW total power) process sheet metal and consumer scrap with consistent throughput.
- 3 mm to 6 mm Mixed Plate and Tubing: Requires heavy-duty drive packages (90 kW to 160 kW) with forged alloy shafts and hardened multi-hook knives.
- Exceeding 6 mm or Solid Sections: Outside the envelope of dual-shaft shredders; requires heavy hydraulic guillotine shears or heavy-tonnage shear balers.
3. Throughput Volume Demands
Small to medium recycling operations processing 3 to 8 tons per hour operate efficiently with medium dual-shaft shredders. If your facility processes 15 to 40 tons per hour of mixed scrap, a dedicated slow-speed single-shaft or twin-shaft pre-shredder must be positioned ahead of high-speed hammer mills to pre-cut feedstock and protect downstream equipment.
4. Upstream Preparation Best Practices
For yards processing automotive scrap, implementing a standardized depollution and pre-shearing stage extends shredder blade life significantly: – Remove engines, transmissions, and drive axles using an excavator equipped with a rotating hydraulic grapple or mobile scrap shear. – Cut large body pillars and solid bumper reinforcements with a stationary alligator shear before hopper loading. – Evacuate all fluids, refrigerants, and hazardous batteries before feeding.
By matching your scrap profile to the correct machine size and enforcing strict pre-sorting protocols, you protect your capital investment and maintain predictable processing margins.
Key Takeaways
Pre-sort solid automotive drivelines, limit feedstock to sheet metal under 4 mm, and deploy hydraulic alligator shears upstream to maximize dual-shaft shredder throughput and cutter life.
— YOUR RECYCLING PROJECT
Find the right machine for your material.
Tell us your material and required capacity.
Or email sales@mecuvo.com