Table of Content
When purchasing replacement knives or evaluating a new copper granulator, buyers encounter massive price variations: a set of cheap 9CrSi blades costs $350, while premium JIS SKD-11 or AISI D2 blades cost $900. A metallurgical wear-life analysis proves that cheap 9CrSi blades dull within 40 operating hours and incur over $4,500 in annual resharpening downtime, whereas vacuum heat-treated SKD-11 blades maintain razor-sharp shearing edges for 280 to 350 hours, delivering five times lower cost per ton processed. Examining Rockwell hardness, carbide microstructure, friction thermal degradation, and life-cycle sharpening costs demonstrates why tool steel metallurgy determines your plant’s operating margin.
What is the metallurgical difference between 9CrSi, Cr12MoV, and D2/SKD-11?
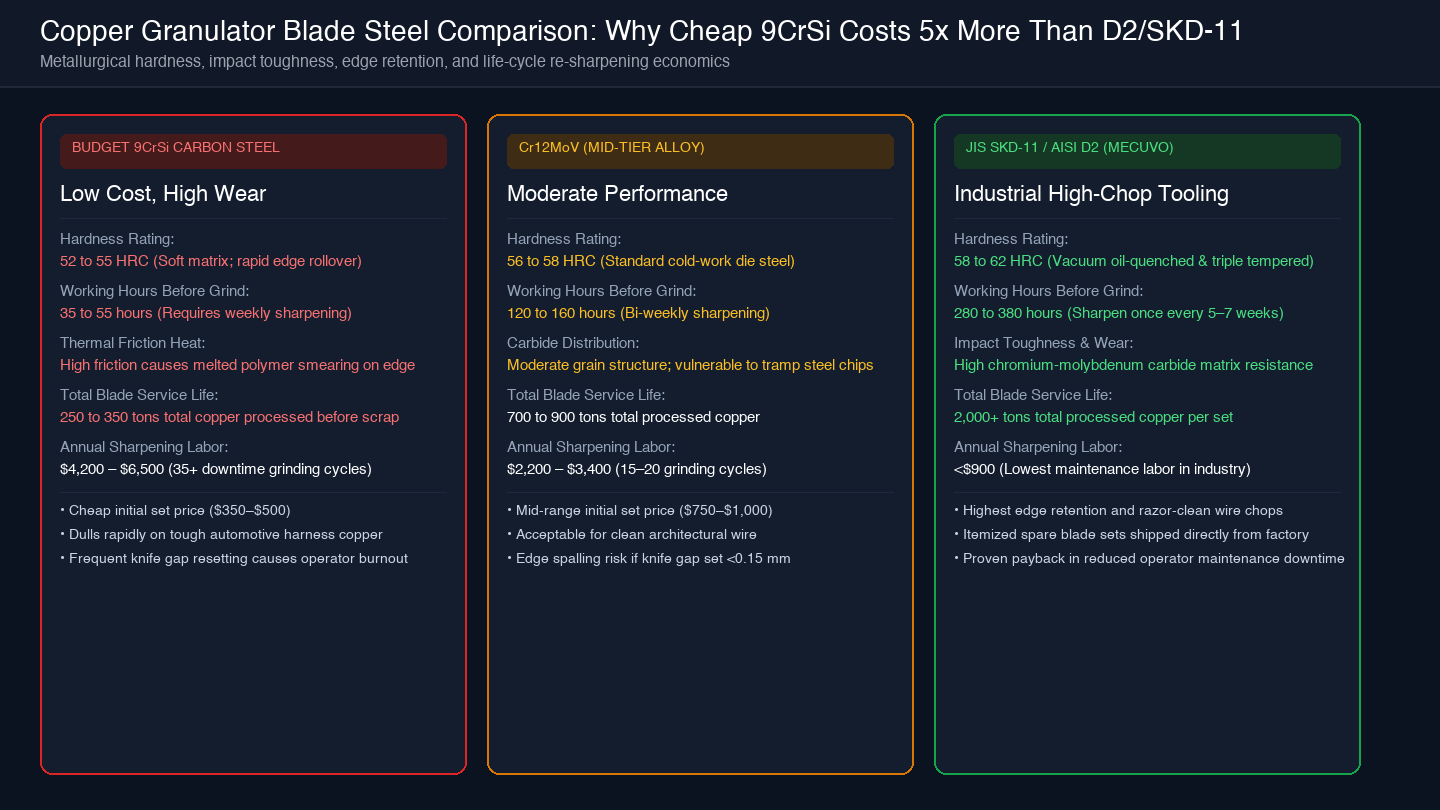
I analyze the alloy chemistry, chromium carbide matrix, and heat treatment processes of common knife steels. Budget 9CrSi is a low-alloy carbon steel (52–55 HRC) that softens under frictional heat, whereas JIS SKD-11 / AISI D2 contains 12% chromium and 1% molybdenum (58–62 HRC), creating dense wear-resistant carbides.
Chemical composition breakdown, carbide volume fraction, and Rockwell hardness (HRC)
The ability of a knife edge to shear tough, work-hardening ductile copper scrap depends directly on alloy chemistry:
- 9CrSi (Low-Alloy Carbon Steel): Contains 0.85–0.95% Carbon and only 0.90–1.20% Chromium. It achieves a surface hardness of only 52 to 55 HRC. Because it lacks secondary carbide-forming elements (molybdenum and vanadium), it has low red-hardness. When cutting wire friction heats the blade edge above 150°C, the steel tempers back and softens rapidly.
- Cr12MoV (Mid-Grade Cold-Work Steel): Contains 1.45–1.70% Carbon, 11–12.5% Chromium, and 0.40–0.60% Molybdenum. Achieving 56 to 58 HRC, it offers fair abrasion resistance but has uneven carbide distribution, making it vulnerable to chipping on hard tramp wire.
- JIS SKD-11 / AISI D2 (The Commercial Standard): Contains 1.40–1.60% Carbon, 11.5–13.0% Chromium, 0.80–1.20% Molybdenum, and 0.20–0.50% Vanadium. Processed via vacuum oil quenching and triple high-temperature tempering, it achieves 58 to 62 HRC. Dense complex chromium-molybdenum carbides resist abrasive wear while retaining superior toughness.
How do blade wear curves impact cutting hours and copper granulation quality?
I examine the correlation between blade sharpness degradation, plastic smear melting, and copper nodule quality. Dull 9CrSi blades roll edges after 40 hours, generating excessive frictional heat that smears molten plastic onto copper granules; SKD-11 maintains sharp shearing edges for 300+ hours, producing clean, unsmudged chops.
Edge radius degradation, frictional thermal smearing, and work-hardening copper
Blade degradation creates a cascading series of operational failures:
- Edge Rollover vs Clean Shearing: Sharp tool steel shears copper wire crisply with minimal deformation. As softer 9CrSi edges wear, the cutting edge radius expands from 0.02 mm to over 0.20 mm. Instead of shearing, the blade begins pinching and smearing ductile copper against the stationary bed knife.
- Frictional Heat & Polymer Smearing: Pinching generates extreme friction, driving cutting chamber temperatures above 115°C. At this temperature, PVC and PE insulation melt into a sticky film that coats the blades and blinds the screen perforations.
- Work-Hardening Effect: Ductile copper work-hardens when repeatedly deformed by blunt knives, increasing cutting torque demands and tripping main drive motor overloads.
What is the true life-cycle cost comparison including resharpening downtime?
I calculate the complete 12-month financial equation including blade purchases, surface grinding fees, and lost production. Over one year of processing 25 tons monthly, cheap 9CrSi blades accumulate $5,650 in sharpening fees and downtime, whereas SKD-11 blades cost just $1,850 total—saving $3,800 annually per machine.
Maintenance labor accounting, precision wet surface grinding, and knife gap re-shimming
Review the real-world operational economics across 2,000 annual working hours:
| Operating Metric | Cheap 9CrSi Steel | JIS SKD-11 / AISI D2 (MECUVO) |
|---|---|---|
| Initial Blade Set Cost | $350 | $850 |
| Operating Hours Between Grinds | 45 Hours | 320 Hours |
| Sharpenings Required per Year | ~44 Times | ~6 Times |
| Professional Grinding Cost (@ $65/set) | $2,860 / Year | $390 / Year |
| Operator Labor to Swap & Shim (2 hrs @ $30/hr) | $2,640 / Year | $360 / Year |
| Annual Blade Replacement Sets | 3 Sets ($1,050) | 1 Set ($850) |
| Total Annual Tooling Overhead | $6,550 / Year | $1,600 / Year |
| Net Annual Operational Savings | Baseline | +$4,950 Saved / Machine! |
Investing in premium SKD-11 blades pays for itself within the first three months purely through eliminated maintenance labor.
How should operators sharpen and gap SKD-11 blades to maximize service life?
I provide precise knife setting instructions using feeler gauges and wet magnetic surface grinding guidelines. Always sharpen blades using flood coolant to prevent thermal micro-cracking, maintain a 35–42 degree cutting bevel angle, and calibrate rotor-to-bed knife clearances strictly to 0.15–0.20 mm.
Flood coolant surface grinding, micro-crack prevention, and feeler gauge gap setting
To ensure your SKD-11 knives achieve 2,000+ tons of processed copper over their lifespan, adhere strictly to these maintenance rules:
- Flood Coolant Surface Grinding: Never dry-grind tool steel knives on an offhand pedestal grinder! Dry grinding induces localized thermal shock exceeding 700°C, creating microscopic surface craze cracks that propagate into catastrophic blade fractures under load. Use a magnetic chuck surface grinder with heavy water-soluble flood coolant.
- The 0.15 mm – 0.20 mm Clearance Rule: Set knife gap using non-magnetic brass feeler gauges across the entire blade length (left, center, and right). A clearance tighter than 0.12 mm risks thermal blade clash as parts expand; a gap wider than 0.25 mm causes thin hair wire to fold and jam.
- Torque Wrench Tightening: Always torque knife clamping bolts in a crisscross sequence using high-tensile Grade 12.9 socket head bolts to 140–160 Nm to prevent blade movement.
Equip Your Facility with Genuine SKD-11 Tooling from MECUVO
- Free Factory Sample Testing: Ship 20–50 kg of your scrap wire to MECUVO. We will run it on our SKD-11 equipped cutting mills and return clean, unsmudged copper chops along with a certified test video.
- Custom ROI & Payback Spreadsheet: Contact MECUVO engineering to receive an automated tooling wear calculator tailored to your wire types.
- Direct Factory Price & Spec Sheet: View complete machine configurations and order spare vacuum-hardened SKD-11 blade sets directly from our MECUVO copper granulator machines overview page.
Key Takeaways
Cheap 9CrSi blades dull in 40 hours and cost $6,500+ annually in maintenance overhead; vacuum heat-treated SKD-11 blades deliver 320+ cutting hours, clean unsmudged copper, and save nearly $5,000 per machine every year.
— YOUR RECYCLING PROJECT
Find the right machine for your material.
Tell us your material and required capacity.
Or email sales@mecuvo.com